In many industrial applications, rubber conveyor belts are indispensable. They carry material at high velocities in various production areas. These systems minimize the use of manual labour for more efficient work performance in the workplace. Conveyor belts are used in a variety of applications in industries. They are used in the mining, manufacturing, agriculture, and logistics industries. Strength – rubber conveyor belts are still in use today. They are capable of bearing high weight and working in tough conditions.
A rubber conveyor belt is a belt made of rubber.
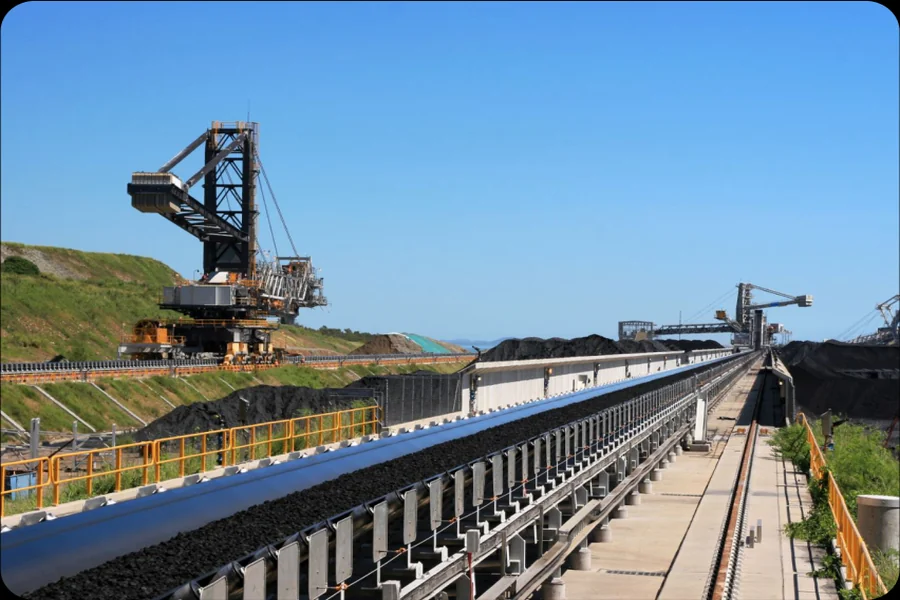
A rubber conveyor belt is a conveyor belt system that conveys materials continuously. Typically has a string material of rubber that is durable in nature. When working, the belt spins around rotating pulleys. The continuous movement is caused by these pulleys operating on the conveyor frame. From then on, materials can be moved from one place to another.
Existing parts are also shown in green.
A conveyor belt made of rubber has many components that are important. The belt moves the materials when the material is being transported. The force for moving a belt is available in the Drive Pulleys. The belt is assisted in going around the system by tail pulleys. The rollers help to maintain the belt in place and prevent any friction that wouldn’t be necessary.
How?
A conveyor belt made of rubber moves continually in a mechanical process. The power from the motor is passed on to the drive pulley. The pulley then pulls the conveyor belt towards it. The belt rests on the rollers to pass along the rest of the frame.
The moving belt surface is loaded with materials by the workers. These materials are pushed towards the discharge point by the belt. The materials are then taken out of the conveyor system. This process can be a continuous one throughout the production process.
Why are rubbers widely used on conveyor belts?
Rubber conveyor belting offers a number of key advantages in industries. They can be constructed in a flexible manner so that they can move continuously around pulleys. May be used with a variety of materials and loads as well. A wide variety of rubber belts offer abrasion resistance.
Rubber also offers some benefit when handling materials as it is impact resistant. This option is useful in the mining and heavy industries. Heavy and sharp materials produce great impact forces. These challenging conditions are handled nicely with durable rubber construction.
Rubber Conveyor Belts are used in a wide variety of applications.
Rubber conveyor systems are employed in many industries to convey materials. They are used in the mining industry to service shuttle trucks and shovel buckets. Mining applications include using them to power shuttle trucks and shovel buckets. Sand and Aggregate handling is done by Conveyors in construction companies. Manufacturing plants transport products from one stage in the manufacturing process to another.
Other industries rely heavily on conveyor systems, too, as they are found in many agricultural enterprises. They are able to move grain, feed, and harvested products effectively and efficiently. Conveyor belts are also used for sorting and carrying packages from one warehouse to another. They are also used for transporting recyclable materials to recycling facilities.
Understanding and selecting the right rubber conveyor belt.
It is important to deliberate on the proper conveyor belt choice. The first thing considerations for a business is to take into account the material that is being moved. The belt strength may be influenced by the weight of the material. The size of the material may also affect the needs for the construction of belts.
Another important factor is its operating temperature. In some applications, extremely hot or cold environments are encountered. Rubber belt performance can also be affected by exposure to chemicals. Belts can be made specifically for more challenging applications.
There are several advantages to rubber conveyor belts.
Rubber conveyor belts can boost productivity remarkably in the workplace. They limit the need for manual transportation of materials. When a work area has no humans in it, automated movement may additionally counteract physical stress on workers. They can help ensure consistent production processes through continuous operation.
Such belts are capable of long-range transportation of materials. They are able to transfer materials from one level of production to the next in the production process. They can be used in numerous industries due to their versatility. They can be improved even more when properly maintained.
Maintenance and Care
Rubber conveyor belts are easier to maintain with regular maintenance such as that available at https://rentonebelt.com/. Anyone who works with a belt should regularly check belts for visible damage. Advise them to look out for cracks, cuts, and excessive wear. Regular attention should also be paid to proper belt alignment.
Cleanliness and correct alignment of pulleys and rollers are essential. When an excessive buildup occurs on a conveyor, it may affect the conveyor’s performance. Belt tension should also be checked on a regular basis by workers. Timely maintenance can be helpful to avoid costly repairs.
Optimisation of the Efficiency of Conveyor Belt.
Purchasing the right conveyor system is essential to proper conveyor operation. Companies have to use belts as per their applications. Efficient energy usage can be made possible through correct belt tension. Proper alignment can minimize unproductive wear of components as well.
Today’s conveyor systems can be equipped with automated monitoring technology. Sensors are able to detect belt movement and any malfunction. Monitoring systems can be used to detect potential issues at a young age. This will help minimise unexpected production stoppages.
Conclusion
Rubber conveyor belts are suitable for conveying materials in industrial settings smoothly and effectively. They are constructed with a certain durability to meet the requirements of industrial applications. However, make use of pulleys, tension systems, motors, and rollers at the same time. The materials move continuously and in a controlled manner as a result of these components.
The proper use of belts results in better performance and service life. Another benefit of regular inspection is that you can prevent unexpected equipment failures. Rubber conveyor systems can be incorporated into several applications in business. They are still a critical solution in today’s material handling.
This can be helpful when considering a conveyor belt solution, or the equipment itself, as this should be covered when connecting with a company like Click for More, which is investigating the options and applications that are available for them.